Welcome to visit
Choosing a magnetic cylinder is not only about diameter and magnetic force. Learn the 6 critical factors that affect rotary die-cutting accuracy, machine compatibility, flexible die performance, and long-term production stability.
In rotary label die cutting, a magnetic cylinder may look like a relatively simple precision component. However, selecting the right cylinder involves much more than matching its diameter and overall length.
A magnetic cylinder must work accurately with the press, gear system, flexible die, anvil cylinder, and the actual converting material. If any of these elements are mismatched, the cylinder may still fit the machine, but problems can appear during production, including inconsistent cutting depth, premature flexible die wear, unstable high-speed operation, or damage to the liner.
For this reason, buyers should evaluate several technical factors before ordering a new magnetic cylinder or replacing an existing one.
1. Machine Brand and Model Should Be Confirmed First
The machine brand and model are among the most important pieces of information when selecting a magnetic cylinder.
Different flexographic presses and rotary die-cutting machines may use different shaft designs, bearer dimensions, gear positions, mounting structures, and working widths.
Two magnetic cylinders may look very similar but still be completely incompatible.
When replacing an existing cylinder, the most reliable references are usually:
Machine brand and model
Existing cylinder drawing
Old cylinder dimensions
Photos of the gear side and shaft structure
If the original drawing is available, it is generally preferable to measuring a heavily used cylinder, because wear can affect some of the measured dimensions.
The objective is not simply to produce a cylinder that looks similar to the original one. It must match the mechanical and transmission requirements of the machine.
2. Repeat and Gear Teeth Must Match the Press
In rotary die cutting, the cylinder circumference determines the repeat length of the job.
The repeat is directly related to cylinder diameter, gear teeth, and the pitch system of the machine.
This is why providing only a cylinder diameter is often not enough.
Important information can include:
Repeat length
Number of gear teeth
Gear pitch or specification
Cylinder diameter
Existing cylinder reference
When replacing a magnetic cylinder, the gear teeth and gear specification must match the press correctly.
A cylinder that physically fits into the machine but has an incorrect gear configuration can create running problems, registration issues, or unstable die-cutting performance.
For plants operating multiple presses, it is especially important not to assume that cylinders are interchangeable simply because their working widths or outside dimensions appear similar.
3. Working Width Is Not the Same as Overall Length
One of the most common sources of confusion when discussing magnetic cylinder dimensions is the difference between:
Working Width, Face Length, and Overall Length.
These measurements describe different parts of the cylinder.
The working width refers to the usable magnetic area where the flexible die is installed. The overall length may also include bearers, shaft sections, gears, or other mechanical features.
For an existing machine, following the original cylinder dimensions is usually the safest approach.
For a new project, working width should be determined according to:
Maximum web width
Actual die-cutting area
Flexible die layout
Maximum converting width of the machine
A wider magnetic face is not automatically better. Excessive width may increase cylinder weight and cost without providing any real production benefit.
4. Magnetic Force Is Important, but Mechanical Accuracy Matters More Than Many Buyers Realize
Magnetic force is naturally important because the flexible die must remain securely attached to the cylinder during operation.
However, magnetic strength alone does not determine the quality of a magnetic cylinder.
Mechanical accuracy is equally important.
Key factors include:
Total indicated runout
Concentricity
Bearer accuracy
Cylinder diameter accuracy
Gear accuracy
Uniform magnetic holding force
Once a flexible die is installed, it rotates together with the magnetic cylinder at production speed.
If the cylinder has excessive runout, the distance between the cutting edge and the anvil cylinder changes during every revolution.
The result may be uneven cutting depth across the repeat.
In practice, this can appear as a job where one area cuts correctly while another area either cuts too deeply or does not cut completely.
For high-speed label production, repeatable mechanical accuracy is therefore more important than simply comparing the number of magnets or maximum magnetic force.
5. The Magnetic Cylinder, Flexible Die, and Anvil Cylinder Must Be Considered as One System
A magnetic cylinder does not perform die cutting by itself.
The actual cutting system consists of:
Magnetic Cylinder + Flexible Die + Anvil Cylinder
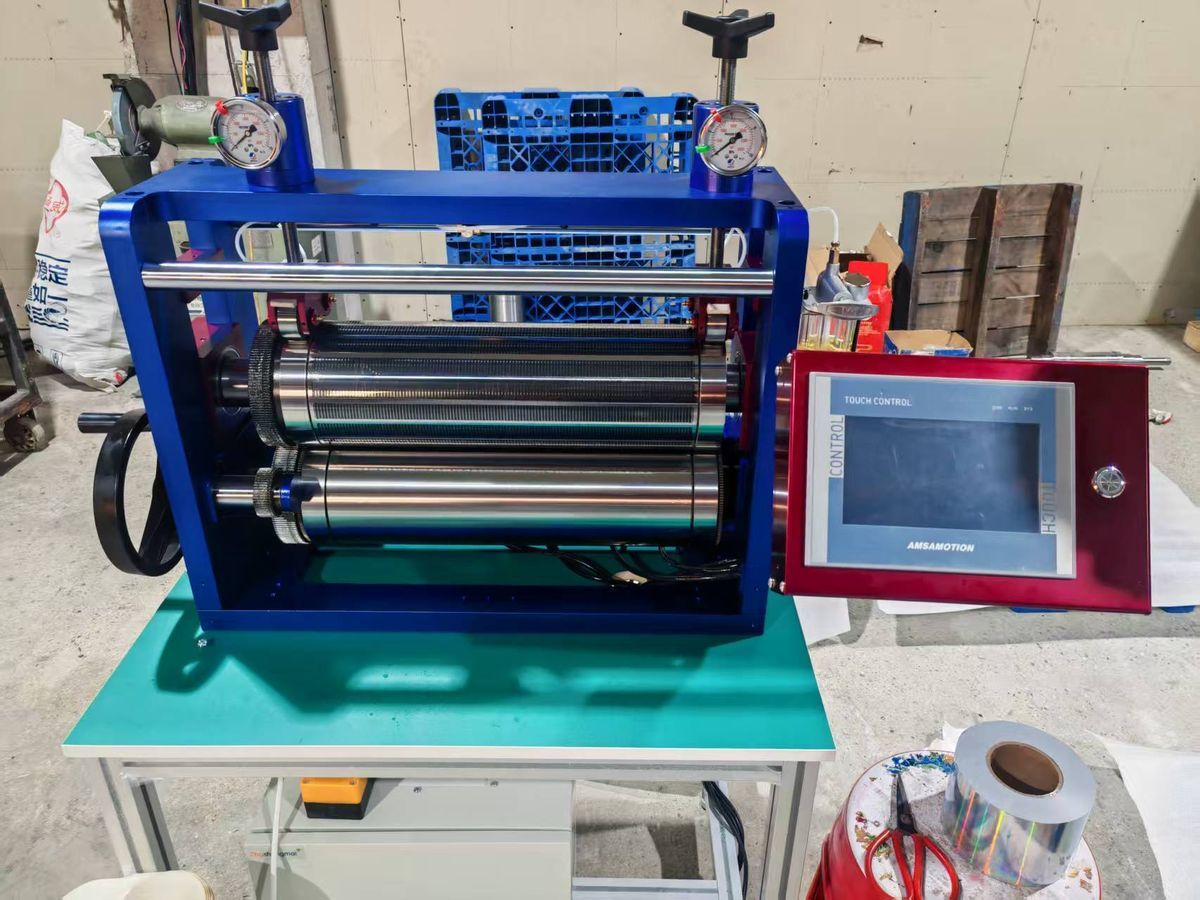
The flexible die is mounted on the magnetic cylinder, while the anvil cylinder supports the substrate during cutting.
Final cutting performance is influenced by several factors, including:
Flexible die thickness
Cutting height
Anvil cylinder condition
Bearer condition
Cutting clearance
Substrate and liner thickness
Machine pressure
This becomes particularly important when converting thin liners, film labels, or PET liners.
These materials often have a narrower cutting tolerance.
The face material must be cut cleanly, while damage to the liner must remain minimal.
If the magnetic cylinder has excessive runout or the anvil cylinder is worn, the cutting window becomes even more difficult to control.
For this reason, persistent die-cutting problems should not always be blamed on the flexible die alone.
The magnetic cylinder and anvil cylinder should also be considered when cutting depth becomes inconsistent.
6. OEM Magnetic Cylinder Replacement Requires More Than Copying the Outside Dimensions
Many label converters eventually need to replace an original magnetic cylinder after years of production.
OEM replacement can be a practical option, but only when the critical dimensions and mechanical features are matched correctly.
Typical parameters include:
Cylinder diameter
Repeat
Gear teeth
Gear specification
Working width
Bearer diameter
Shaft structure
Overall length
Existing drawing or sample dimensions
The most important point is that an OEM magnetic cylinder should not simply be “close” to the original size.
Its key mechanical dimensions must correspond correctly with the machine.
When an old cylinder has already experienced significant wear, some measured dimensions may no longer represent the original specification.
Whenever possible, original technical drawings or reliable historical specifications should be used together with physical measurements.
Frequently Asked Questions
Is stronger magnetic force always better?
No.
The magnetic force must be strong enough to hold the flexible die securely, but excessive focus on magnetic strength alone can be misleading.
Uniform magnetic holding force and mechanical accuracy are more important than simply having the strongest possible magnet system.
A cylinder with strong magnetic force but poor concentricity or excessive runout can still produce inconsistent die-cutting results.
Can a magnetic cylinder be manufactured without the original drawing?
Yes.
If the original drawing is not available, the cylinder can often be evaluated based on the machine model, old cylinder dimensions, gear information, working width, and clear photos of the shaft and mounting structure.
However, the more complete the dimensional information, the lower the risk of mismatch.
Why can two magnetic cylinders with the same dimensions perform differently?
Because outside dimensions are only part of the specification.
Differences in runout, concentricity, bearer accuracy, gear quality, surface machining, and magnetic force distribution can all affect the final die-cutting result.
These differences become more noticeable at higher machine speeds or when working with thin liners and demanding label materials.
Why does PET liner require better die-cutting accuracy?
PET liner usually provides a smaller margin for cutting error than standard paper liner.
The cutting edge must penetrate the face material correctly without excessively marking or cutting through the PET liner.
This requires more stable control of the cutting clearance between the flexible die and the anvil cylinder.
For this reason, magnetic cylinder accuracy, anvil condition, flexible die quality, and press setup all become more critical.
How often should a magnetic cylinder be replaced?
There is no fixed replacement interval.
Service life depends on machine speed, operating hours, maintenance, bearer wear, flexible die handling, and whether the cylinder has experienced impact or abnormal pressure.
If a previously stable production process begins to require more frequent pressure adjustment, or cutting depth becomes inconsistent across the web, checking cylinder runout and bearer condition is recommended.
Conclusion
Selecting a magnetic cylinder should never be based only on price, diameter, or magnetic force.
For reliable rotary label die cutting, the most important factors are:
machine compatibility, repeat, gear specification, working width, mechanical accuracy, and proper interaction with the flexible die and anvil cylinder.
Providing the machine model, original cylinder drawing, or accurate dimensions before production can reduce the risk of specification errors and help ensure that the replacement cylinder runs correctly from installation.
For label converters using flexible dies in high-speed production, a precisely manufactured magnetic cylinder is not simply a spare part. It is a key component in maintaining stable cutting quality, reducing setup adjustments, and supporting consistent production over the long term.