Welcome to visit
In flexographic printing, if the printed web shows transverse light-and-dark stripes that run across the web direction and repeat at regular intervals, operators often begin by checking ink viscosity, doctor blade settings, the anilox roll, or printing pressure.
However, when these stripes are clearly periodic—especially when they are less visible at low speed but become more pronounced as press speed increases—the problem may not be related to the ink or printing plate. It may instead be connected to the flexo plate cylinder, drive gear, or the mechanical accuracy of the printing unit.
Repeatedly increasing impression pressure or reducing press speed may only mask the symptom temporarily. It does not eliminate the underlying mechanical cause.
1. First, Determine Whether the Stripes Follow a Mechanical Repeat Pattern
The first step is to observe whether the defect follows a consistent pattern.
Check the following:
Is the distance between adjacent stripes approximately the same?
Does the defect repeatedly appear in the same position?
Does it become more visible as press speed increases?
Does the defect become less severe when the press is slowed down?
Does the repeat frequency correspond to the gear pitch or plate cylinder rotation?
If the defect repeats at a fixed interval, it often indicates that the problem is related to a rotating component or a mechanical transmission cycle.
At this stage, the flexo plate cylinder, gear, bearings, and related drive components should be included in the troubleshooting process.
2. Check Whether the Flexo Plate Cylinder and Gear Are Correctly Matched
On gear-driven flexographic presses, the plate cylinder dimensions and the drive gear must maintain the correct mechanical relationship.
If the actual working diameter of the flexo plate cylinder does not correctly match the pitch diameter of the gear, a slight difference in surface speed may occur between the plate cylinder, impression cylinder, and substrate.
At higher press speeds, this mismatch can create periodic squeezing, slipping, or vibration, which may appear on the printed web as:
Repeating transverse stripes
Gear marks
Periodic light-and-dark density variation
Dot slur or deformation
Unstable printing pressure
If the problem begins after replacing a plate cylinder, gear, or related component, the plate cylinder diameter, gear specification, number of teeth, and actual operating conditions should be checked carefully.
3. Do Not Ignore Gear Wear and Gear Mesh Conditions
Even when the plate cylinder dimensions are correct, abnormal gear conditions can still create repeating print defects.
Check for:
Visible wear on the gear teeth
Ink, dust, or debris inside the gear teeth
Insufficient lubrication
Gear mesh that is too tight or too loose
Excessive backlash
Gear runout or improper installation
Periodic noise or vibration during operation
On older flexographic presses, a gear may not appear seriously damaged during a static inspection. However, minor wear and gear-mesh errors can become much more significant at higher operating speeds and reduce print stability.
4. If the Gear Is Normal, Check Plate Cylinder TIR and Concentricity
If no obvious gear problem is found, the next step is to inspect the mechanical accuracy of the flexo plate cylinder itself.
Key items to check include:
Finished plate cylinder diameter
TIR (Total Indicated Runout)
Concentricity
Journal accuracy
Bearing fit and bearing locations
Local deformation of the cylinder body
Abnormal vibration at higher operating speeds
If the plate cylinder has excessive runout, the actual impression between the printing plate and substrate may change during every revolution.
When plate cylinder runout and gear-related vibration occur together, transverse stripes can become even more pronounced.
For this reason, a repeating print defect should not be diagnosed by checking the gear alone. The running accuracy of the flexo plate cylinder must also be evaluated.
5. Why Increasing Impression Pressure Is Usually Not the Right Solution
When transverse stripes appear, a common response is to increase impression pressure.
This may temporarily improve areas with insufficient impression, but if the root cause is plate cylinder runout, improper gear mesh, or a mechanical mismatch, additional pressure does not solve the actual problem.
Excessive impression pressure can instead lead to:
Increased dot gain
Excessive plate compression
More visible gear marks
Shorter plate and mounting tape life
Greater vibration at higher press speeds
A more effective troubleshooting sequence is:
Defect repeat pattern → Impression pressure → Gear condition → Gear-to-cylinder matching → Plate cylinder TIR and concentricity → Journals and bearings
When Should You Consider Replacing the Flexo Plate Cylinder?
If the ink, printing plate, anilox roll, and normal impression settings have already been ruled out, and further inspection shows excessive TIR, poor concentricity, journal wear, cylinder deformation, or an incorrect gear-to-cylinder relationship, continuing to compensate by press adjustment or lower operating speed may only provide temporary relief.
For older plate cylinders whose mechanical accuracy can no longer be restored reliably, replacing the cylinder with a new flexo plate cylinder manufactured according to the original technical drawing and actual operating conditions is often the more stable long-term solution.
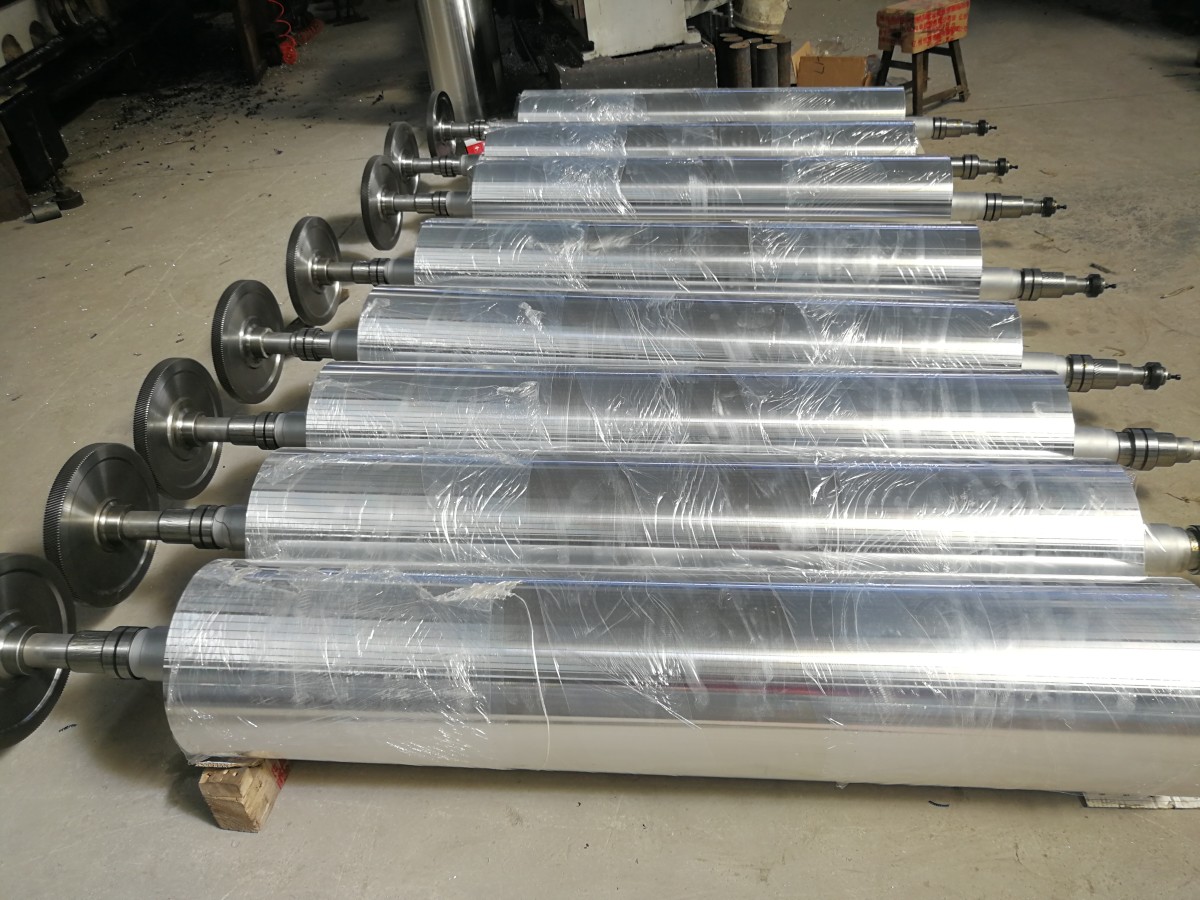
Before manufacturing a new flexo plate cylinder, key parameters should be confirmed, including the technical drawing, cylinder diameter, gear specification, TIR, concentricity, journal dimensions, and operating speed. This helps reduce the risk of repeating the same mechanical compatibility problems after installation.
If your flexographic press is experiencing repeating transverse stripes, gear marks, or unstable print quality at higher speeds, and you suspect the plate cylinder may be involved, you can send us the plate cylinder drawing, press model, and a description of the current printing problem.
We can review your application requirements, confirm the manufacturing specifications for a replacement cylinder, and provide a quotation for a custom flexo plate cylinder.