Welcome to visit
In modern flexographic printing, higher press speeds, shorter changeover times and increasingly demanding print quality requirements are changing the way converters evaluate press components.
The plate mounting sleeve may appear to be a relatively simple part of the flexographic printing system, but its weight, structural stability, dimensional consistency and resistance to the production environment can directly affect day-to-day press operation.
For many years, polyurethane foam, commonly known as PU foam, has been widely used as a supporting material inside flexographic printing sleeves. However, as printing speeds increase and converters place greater emphasis on productivity and durability, alternative sleeve structures are attracting more attention.
One such approach is the use of an aramid honeycomb core.
Sleeve Ultra™, developed by JCTPRINT, applies an aramid honeycomb supporting structure to the flexographic plate mounting sleeve. So how does this structure differ from a conventional PU foam sleeve, and what does it mean for flexographic printers?
Understanding the Structure of a Flexo Plate Mounting Sleeve
A plate mounting sleeve must provide more than the correct outer diameter and printing repeat.
During production, it must maintain its geometry while rotating at high speed, fit correctly on the air mandrel or bridge sleeve, withstand repeated mounting and removal, and resist the effects of ink, solvents and normal production handling.
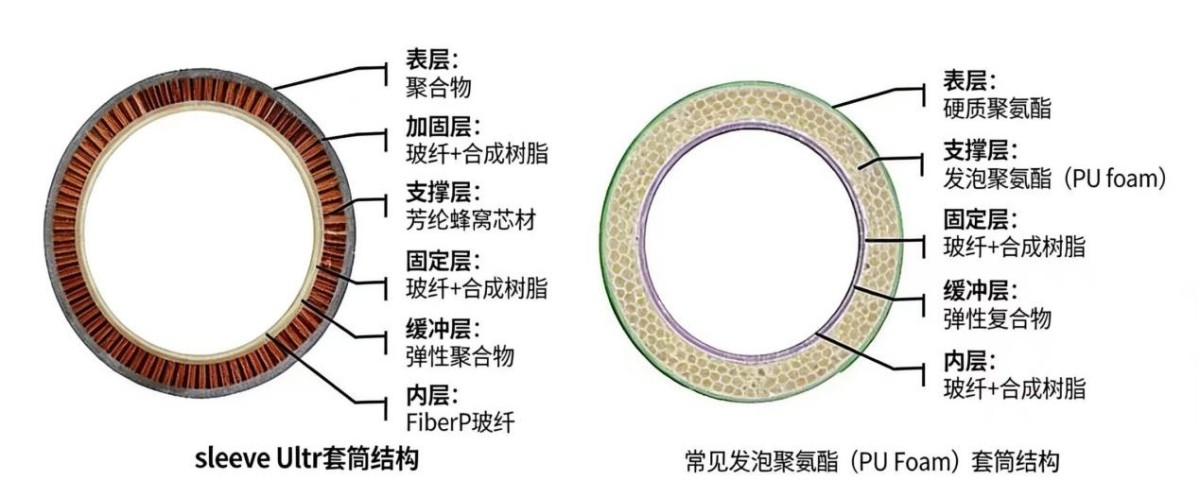
In many conventional plate sleeves, foamed polyurethane is used as an internal supporting layer.
Sleeve Ultra™ takes a different approach. Its supporting structure uses an aramid honeycomb core, combined with a specially manufactured inner layer and external sleeve structure.
The basic design principle is similar to lightweight structural solutions used in demanding engineering applications: reduce unnecessary mass while maintaining structural support.
This difference in internal construction leads to several practical advantages.
1. Significant Weight Reduction
One of the most visible differences between aramid honeycomb and conventional PU foam sleeve structures is weight.
Flexographic sleeves can become relatively heavy when the printing repeat, face length or wall thickness increases. This affects not only the press but also the operators who repeatedly install, remove and transport sleeves during production.
In one Sleeve Ultra™ application, the plate sleeve had the following dimensions:
Inner diameter: 146.539 mm
Sleeve length: 1660 mm
Printing circumference: 680 mm
Single-side wall thickness: 33.5 mm
A conventional sleeve of this specification weighed approximately 19 kg.
The Sleeve Ultra™ version weighed only 11.7 kg.
This represents a weight reduction of nearly 40%.
For printers running multiple job changes each day, reducing sleeve weight can make handling easier and help improve the efficiency of sleeve changeovers. Lower rotating mass can also be valuable as presses move toward faster production speeds and more frequent acceleration and deceleration.
2. Lightweight Does Not Have to Mean Less Stable
Reducing weight is useful only when the sleeve can still maintain the required mechanical stability.
This is one of the main reasons for using a honeycomb structure.
Aramid honeycomb provides a combination of lightweight construction, energy absorption, impact resistance and damping characteristics. Instead of relying primarily on a thicker foam supporting layer, the honeycomb core creates a highly efficient internal supporting structure.
For flexographic printing, this is particularly relevant at higher press speeds.
Sleeve Ultra™ has been operated under 650 m/min high-speed flexographic printing conditions while maintaining physical stability.
For converters considering lightweight plate mounting sleeves, this relationship between weight and stability is important. A sleeve should not simply be lighter; it must remain dimensionally and mechanically suitable for the actual printing conditions.
3. Better Resistance to Ink and Solvent Exposure
The internal material of a plate sleeve is normally hidden during operation, but damage to this layer can eventually affect the entire sleeve.
With conventional PU foam structures, ink or solvent entering through the sleeve end can reach the internal foam layer.
According to the material characteristics used in Sleeve Ultra™ development, foamed polyurethane can be vulnerable when exposed to certain corrosive environments. Damage to the internal supporting material may eventually contribute to changes in sleeve dimensions or reduced compressive performance.
Aramid honeycomb offers stronger resistance to corrosive environments than conventional PU foam.
Sleeve Ultra™ also addresses the problem from another direction: preventing liquids from entering the structure in the first place.
Its SilentShield™ end protection and full-end sealing design is intended to reduce end-face damage and prevent ink or solvents from penetrating into the internal sleeve structure.
The combination of a more resistant supporting material and improved end sealing is designed to support longer-term dimensional and structural reliability.
4. Dimensional Consistency Matters
For professional flexographic printers, sleeve performance is not determined by material alone.
The interface between the sleeve and the mandrel is equally important.
Sleeve Ultra™ uses the FiberP™ inner layer, made from a mixed fiber bundle of glass fiber and high-strength polymer fiber.
The inner layer is manufactured using automated sleeve winding equipment in a controlled temperature and humidity environment. Fiber tension is automatically adjusted, while the winding angle is calculated according to the mandrel diameter.
The purpose of this manufacturing process is to achieve consistent dimensions between sleeves, including sleeves of the same specification produced in different batches.
For the printer, consistent internal dimensions help provide appropriate mounting tightness on both imported and domestic mandrels.
During high-speed printing and rapid acceleration or deceleration, the sleeve must maintain reliable contact with the mandrel or bridge sleeve and avoid unwanted slipping.
This becomes increasingly important as converters push press productivity to higher levels.
5. Impact Protection and Service Life
Plate sleeves are exposed to more than rotational forces.
During everyday production, operators mount, remove, transport and store sleeves repeatedly. The end face is therefore one of the areas most vulnerable to accidental impact.
Damage at the sleeve end may not look serious at first, but it can create a path for ink, cleaning liquid or solvent to enter the internal structure.
Sleeve Ultra™ incorporates the SilentShield™ end design to provide impact buffering while maintaining full-end sealing.
Together with the aramid honeycomb core, this design is intended to reduce internal damage caused by end-face penetration and extend the usable life of the sleeve.
For converters operating a large inventory of printing repeats, longer sleeve life can also reduce replacement frequency and total sleeve management costs.
Aramid Honeycomb vs. PU Foam: Key Differences
When comparing the two structures, several practical differences should be considered.
Weight:
Aramid honeycomb can significantly reduce sleeve mass, particularly in thicker-wall or larger-format sleeves.
Structural support:
The honeycomb structure is designed to provide high support efficiency while keeping overall weight low.
Impact and damping performance:
Aramid honeycomb provides energy absorption, impact resistance and damping characteristics.
Resistance to production environments:
Compared with conventional PU foam, the aramid honeycomb material used in Sleeve Ultra™ provides stronger resistance to corrosive environments.
Long-term structural protection:
When combined with sealed sleeve ends, the structure helps reduce the risk of internal damage caused by ink and solvent penetration.
This does not mean that every flexographic application requires the same sleeve structure.
The correct solution depends on the press, printing repeat, sleeve dimensions, operating speed and production environment. However, for printers focusing on high-speed operation, lightweight handling and long-term sleeve stability, internal sleeve construction deserves much more attention than it often receives.
A New Approach to Flexographic Plate Sleeves
Sleeve Ultra™ was developed as a new-generation plate mounting sleeve for flexographic printing applications.
Its available specification range includes:
Sleeve outer diameter: Ø63–Ø575 mm
Printing circumference: 200–1800 mm
Sleeve length: 300–3000 mm
Single-side wall thickness: 1–100 mm
Antistatic sleeve options available
JCTPRINT also maintains mandrel tooling covering diameters from Ø70.144 mm to Ø490.063 mm, including commonly used sizes such as 105.158 mm, 136.989 mm, 146.539 mm and 156.088 mm.
This allows Sleeve Ultra™ plate mounting sleeves to be customized for a wide range of flexographic printing requirements.
Choosing the Right Plate Mounting Sleeve
When selecting a flexo plate mounting sleeve, price and dimensions should not be the only considerations.
Converters should also evaluate:
sleeve weight,
internal supporting material,
dimensional stability,
mandrel fitting performance,
press operating speed,
resistance to ink and solvents,
end-face protection,
and long-term durability.
As flexographic presses continue to move toward higher productivity, sleeve technology must develop with them.
The transition from conventional PU foam support to an aramid honeycomb sleeve structure represents one possible way to achieve lower weight without sacrificing the structural performance required for modern flexographic production.
If you are evaluating replacement sleeves or developing sleeve specifications for a new flexographic printing project, send us your sleeve inner diameter, printing repeat, face length and press model.
The JCTPRINT team can evaluate the application and recommend a suitable Sleeve Ultra™ plate mounting sleeve configuration.